Private AI that connects your historian, cameras, lab and maintenance records, spots what is drifting and prepares the decision, inside your plant.
Select a highlighted asset to see the AI at work
Concept photography · illustrative AI overlay
Some of our key industrial partners
The problem
Key problems every industrial operator faces.
Stops cost more every year, experienced people are retiring, and the plant keeps changing under you.
$2.3Mlost per hour of downtime at large automotive manufacturers Siemens, 2024
52.7%less unplanned downtime at manufacturers that rely less on reactive maintenance NIST, 2021
1.9MUS manufacturing jobs could go unfilled by 2033 if workforce gaps persist Deloitte & The Manufacturing Institute, 2024
49 daysaverage lead time to commit MRO purchases in US manufacturing ISM, September 2026
Survey and benchmark figures as published by each source, with their own scope. Not Codvo results.
Unplanned stopsWhat trips next, and when?Costs throughput
Yield and quality driftSame feed, same recipe, different result.Costs margin
Alarm floodsWhich of these alarms actually matters?Costs response time
Expertise walking outThe one person who knows why is retiring.Costs know-how
Nothing touches the DCSNo cloud, no writes to control. Full stop.Costs AI that never ships
Solutions
How we unlock value with AI.
Two ways in. Add AI to the historian and tools your engineers already use, or rebuild a process around AI agents. Both stand on one foundation, inside your plant.
Unit U-200 · Urea synthesis · last 48 hYield −1.6% · night shiftFeed 1,450 t/dMode: read-only
NeIO assistantAdded to your historian · cites every record
Before the dip, R-101 synthesis pressure fell 3.2 bar and the NH3/CO2 ratio drifted to 3.1, both from about 21:40. Cooling-water supply did not change. Lab biuret rose to 0.92% on the 02:00 sample.
Shows what moved together. Confirming the cause stays with the process engineer.
The assistant works inside the historian engineers already use, and shows its answer on the trends.Illustrative
Peopledecide and approveOutside limits · routed to ownerApproved
Shift supervisorApproves set-points
Process engineerOwns the limits
NeIO OSPlans the run and routes every exception to the person who owns it.
Control room · shift channelU-200 set-points approved and applied by the operator. Work order raised for E-204 fouling.No autonomous write-back
Agents do the analysis across your systems. Operators own every change to the plant.
One foundation under bothEach piece answers a problem above.
Physics plus ML prediction
Failure warning with the likely cause, trained on synthetic and physics-based data where history is thin.
Unplanned stops
Optimisation within limits
ML models plus an LP optimiser recommend set-points inside operator-set bounds.
Yield drift
Correlation and root cause
Alarms matched on how the plant connects, cause ranked with evidence.
Alarm floods
Engineering knowledge
P&IDs, datasheets, work history and expert notes linked to each asset and cited.
Expertise walking out
Your boundary
No external network path. Models run on site.
Nothing touches the DCS
Ready-made solutions
Start from a solution already running in production.
Built on NeIO and configured to your plant systems, data and boundary.
AI agent
Quality · Safety · Condition
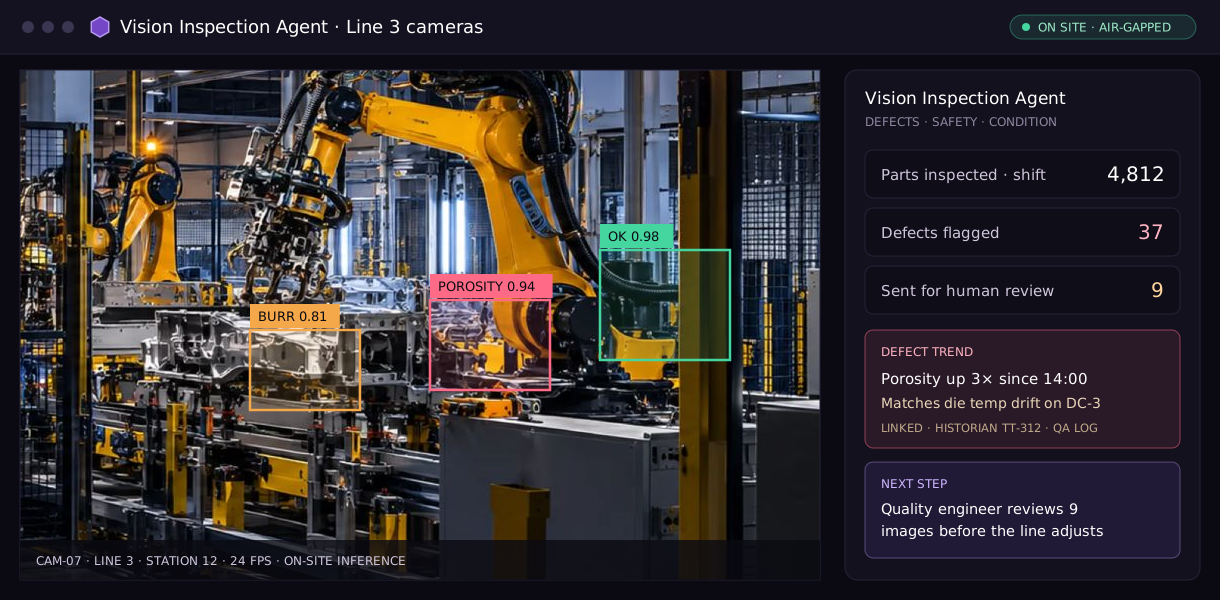
Vision Inspection Agent
Reads line, site and drone cameras on site, finds defects and safety risks, and ranks them for review.
AI agent
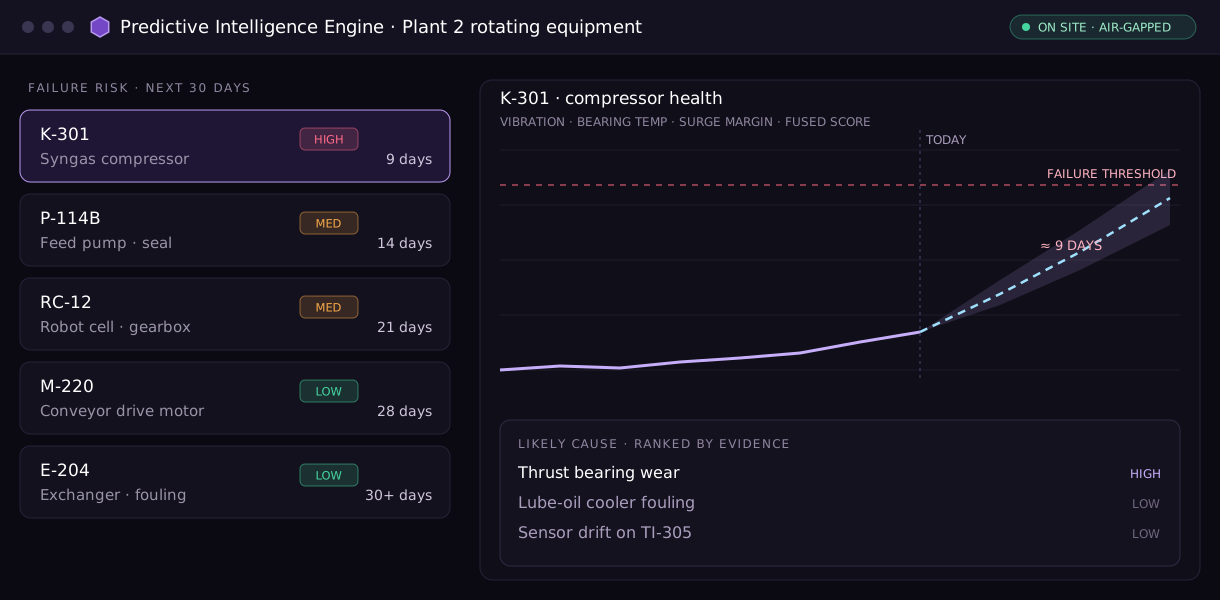
Rotating equipment · Lines
Predictive Intelligence Engine
Predicts pump, compressor, motor and line failures 7–30 days ahead, with the likely cause ranked by evidence.
AI agent
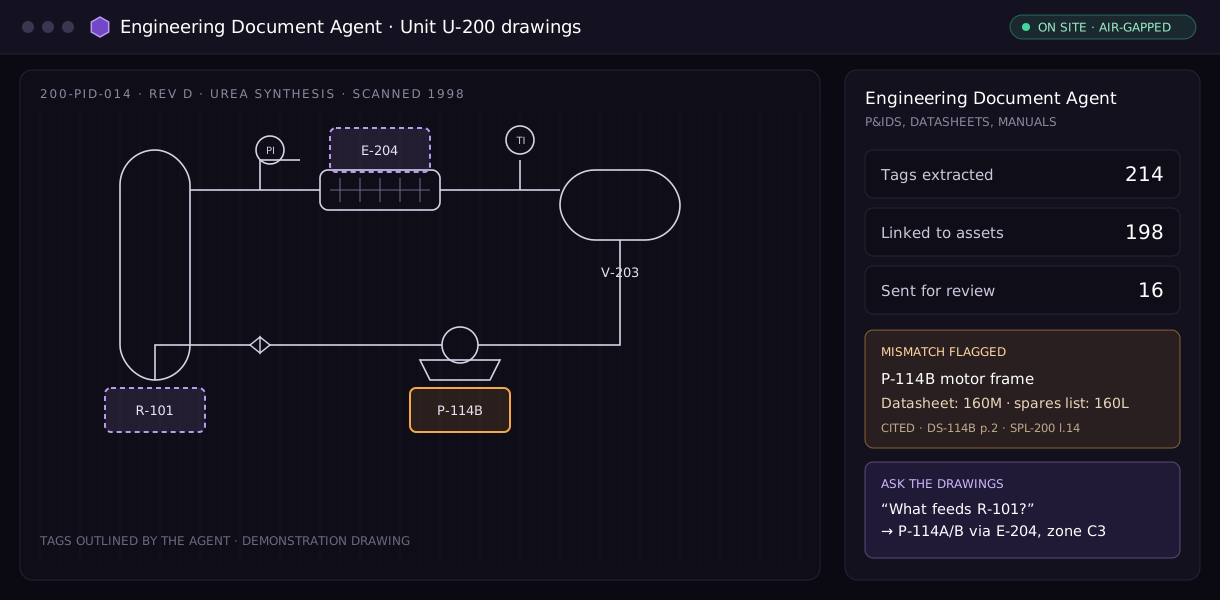
P&IDs · Datasheets · Manuals
Engineering Document Agent
Reads P&IDs, datasheets and manuals, links every tag to its asset and cites the page.
AI agent
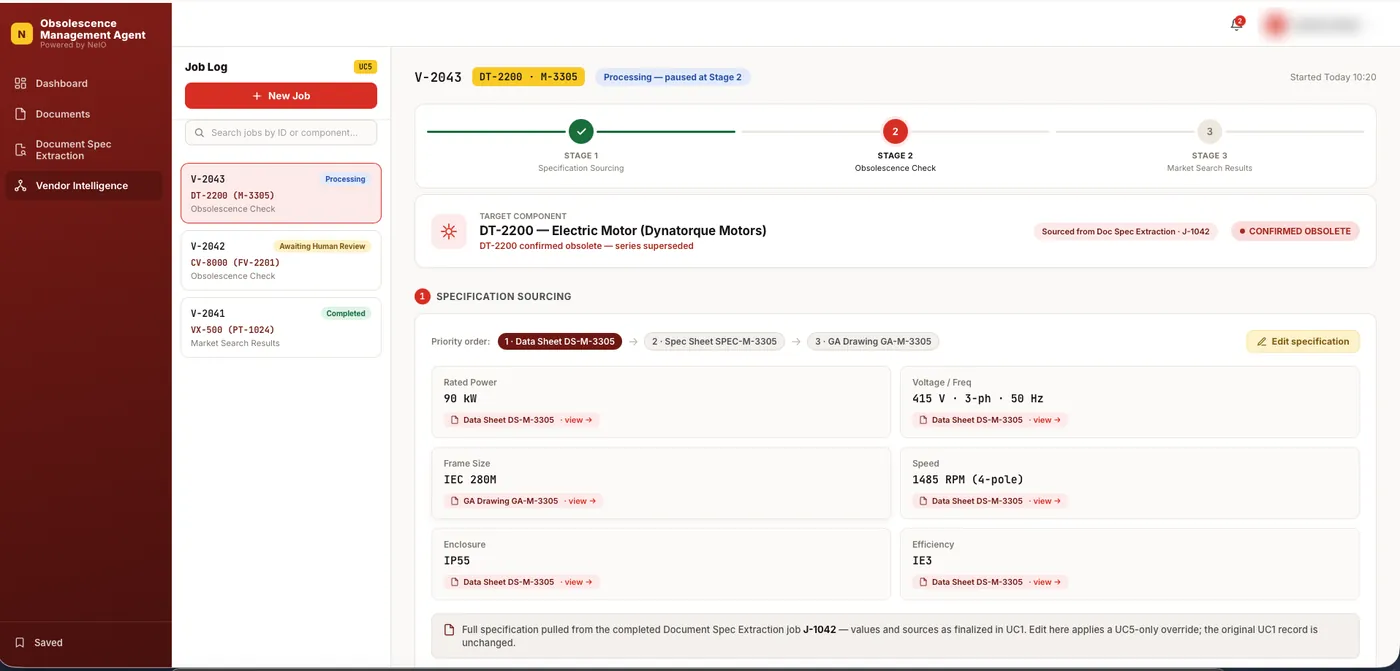
MRO · Spares
Obsolescence Management Agent
Finds unsupported motors, drives and control parts before the reorder fails, with cited alternates.
Illustrative product screens with demonstration data.
Proof
Explore our deployments
Delivered for chemical, semiconductor, mining and industrial technology companies. Client identities are confidential; results are as reported for each engagement.
Chemicals & fertilisers · YieldMiddle East
More saleable product from the same plant
Challenge: No model linked process inputs to yield, and optimisation logic sat inside a third-party platform the client did not control.
What we did: 16 interconnected ML models and an LP optimiser recommending set-points within operator limits, rebuilt as a client-owned platform on-premises.
+2%daily yield against prior operation
16interconnected ML models
Semiconductors · Fab facility operationsRegion TBC
Root cause in minutes, not hours
Challenge: One cooling or power fault set off hundreds of alarms across four facility systems while production was exposed.
What we did: Alarms normalised and de-duplicated, a dependency map of cooling and power paths, and one incident with the cause ranked by evidence. Air-gapped.
<15 minto root cause, was 2–3 hours
1incident instead of hundreds of alarms
Industrial technology provider · Supervisory AISoutheast Asia
From alert to an approved decision, engineer in control
Challenge: Digital-twin outputs had to become decisions engineers could trust and approve.
What we did: A supervisory layer that turns twin outputs into explained recommendations for approval, now part of the provider’s own platform. Local and air-gapped.
30 salert to explained recommendation (design target)
Zerowrites to control systems
Mining · OT data engineeringRegion TBC
One SCADA standard across a mining portfolio
Challenge: Each site had grown its own SCADA conventions, so data could not be compared or reused across mines.
What we did: A common SCADA standard and data model, rolled out mine by mine, so the same analytics and AI run on every site.
17mines on one standard
1data model across sites
Why Codvo
Why Codvo for industrial AI.
We know plants, we already run in them, and we stay after go-live.
01Process and OT nativeHistorians, DCS, LIMS, CMMS and P&IDs, connected around real assets by engineers who know the plant.02Sovereign, no writes to controlOn-site or air-gapped. Recommendations go to operators; nothing writes to the DCS or PLCs.03No cold startPhysics-based and synthetic data train models where real failure history is thin, then calibrate on your plant.04Production, not pilotsRunning in chemical, semiconductor and mining operations, measured against an agreed baseline.
Explore your industrial AI roadmap
Turn plant intelligence into real-world impact.
Bring one yield, reliability, quality or response challenge. In a 45-minute working session we’ll review your environment, show a comparable scenario and agree what a pilot should prove.
 AI agent
 Shift supervisorApproves set-points
 Process engineerOwns the limits
 AI agent
 AI agent
 AI agent